Plainfield Epoxy Flooring installs ESD flooring for facilities in Plainfield, IL, bringing 20+ years of floor coating work to electronics assembly, laboratories, data rooms and equipment spaces, and we also serve surrounding cities including Shorewood, Minooka, North Aurora, Warrenville and Lemont. ESD flooring, short for electrostatic discharge flooring, is designed to carry static charge safely to ground so it does not build up on people and equipment and discharge into sensitive components.
A static spark too small to feel can damage electronics, corrupt data or, in some environments, ignite flammable vapors. An ESD floor is one part of a facility’s static control program, working together with grounded footwear, workstations and procedures, so it has to be specified, installed and tested to meet the plan the facility already follows.
We build ESD floors on the same foundation as every coating we install: mechanical surface preparation, crack repair, moisture testing and a written proposal naming the products, the system build and the finished thickness. The difference is that an ESD floor is not finished when it looks right; it is finished when it measures right.
ESD Standards and Resistance Ranges
ANSI/ESD S20.20 Requirements
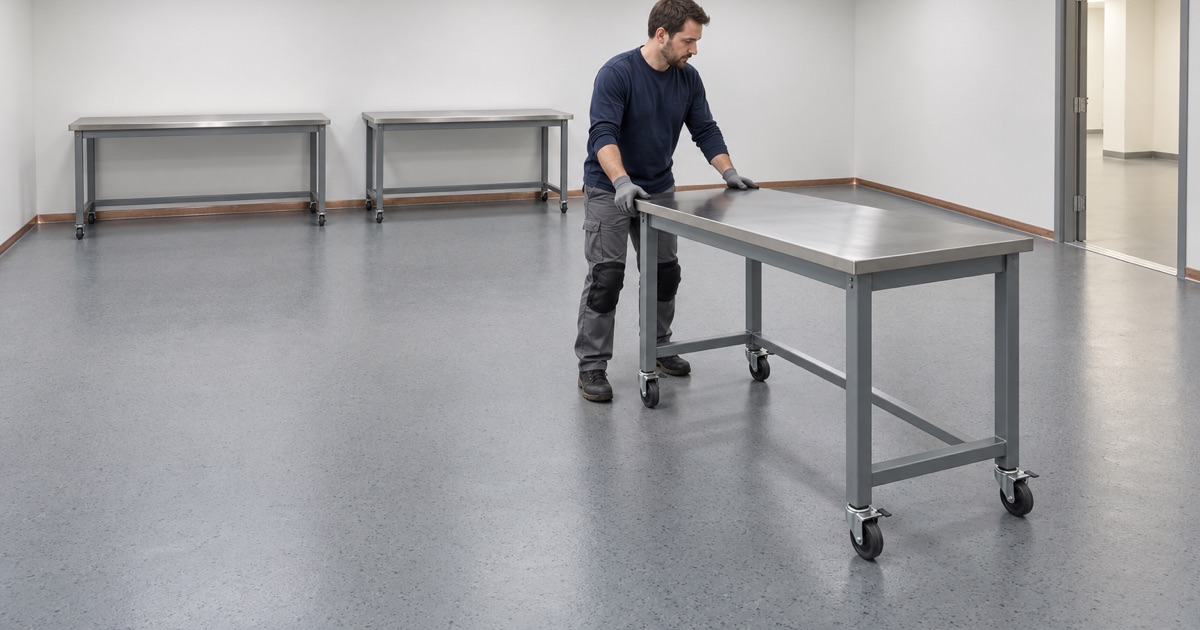
ANSI/ESD S20.20 is the standard most electronics facilities use for static control programs. For flooring, it calls for floor resistance below 1.0 x 10^9 ohms and looks at the floor and footwear as a combined system, limiting the voltage a person wearing approved, grounded footwear can generate while walking to under 100 volts.
Facilities that follow this standard usually have a static control coordinator or quality team who sets the requirements. We work from their specification and confirm the target range before choosing a system.
Conductive Versus Static-Dissipative Floors
Under ANSI/ESD STM7.1, a conductive floor measures below 1.0 x 10^6 ohms, while a static-dissipative floor measures from 1.0 x 10^6 up to, but not including, 1.0 x 10^9 ohms. Conductive floors drain charge faster, and dissipative floors drain it more gradually, and the right range depends on the products being handled and the facility’s own plan.
Choosing the wrong range can create problems. A floor that is too conductive may raise safety concerns around live electrical equipment, while one that is too resistive may not drain charge fast enough to protect sensitive components.
Matching the Floor to the Room
An electronics assembly line, a server room, a lab and a room with flammable vapors each have different needs. We review the specification, the equipment and the traffic in each area before choosing between conductive and static-dissipative systems, and we put the target resistance range in writing in the proposal.
How an ESD Epoxy Floor Is Installed
Surface Preparation and Moisture Testing
We diamond grind or shot blast the slab to a clean, open profile, remove old coatings and sealers, and repair cracks and joints so the system can be applied evenly. We never acid etch, and grinding dust is captured at the tool by vacuum systems so it does not reach sensitive equipment.
The slab is tested for moisture with ASTM F1869 calcium chloride kits or ASTM F2170 relative humidity probes. Moisture can affect both bond and electrical performance, so high readings mean a moisture-mitigation primer is added to the system before the ESD layers go down.
Grounding Points and Conductive Primer
Most ESD epoxy systems use copper grounding strips or grounding points tied into the building’s electrical ground, followed by a conductive primer that links the system together. The number and spacing of grounding points follow the manufacturer’s instructions and the size and layout of the room.
ESD Body Coat and Topcoat
The ESD body coat and topcoat contain conductive additives that create a path for static charge to move from the surface to the grounding points. These coats must be applied at the specified thickness and in even layers, because a thin or uneven area can read outside the target range when the floor is tested.
Testing, Documentation and Maintenance
Resistance Testing After Installation
Once the floor has cured, we test resistance at points across the floor and from the surface to ground using test equipment and methods referenced by the ESD Association standards. Readings are recorded and shared with the facility, giving a baseline that can be compared with later checks.
If any area reads outside the target range, we find out why before the floor is handed over. That might mean extra grounding, a touch-up coat or adjustment in a specific area.
Cleaning ESD Floors
ESD floors should be cleaned with products recommended by the coating manufacturer. Some waxes, polishes and cleaners can leave an insulating film that raises resistance, so the cleaning plan matters as much as the floor itself.
Ongoing Checks
Facilities following ANSI/ESD S20.20 typically check floor performance periodically as part of their static control program. We can provide guidance on testing intervals and what to watch for as the floor ages.
Planning an ESD Flooring Project
Scheduling Around Operations
Electronics plants, labs and data rooms often cannot shut down for long. We schedule ESD floor installation around the facility’s operating hours, including overnight and weekend windows, and plan each phase so sensitive equipment is protected from dust and odors.
Coatings, VOC Limits and Ventilation
Illinois limits the VOC content of floor coatings under 35 Ill. Adm. Code Part 223 Subpart C, and the rule applies to installers as well as manufacturers. We choose compliant ESD products and plan ventilation so the facility can return to work as soon as the floor has cured.
Warranty Terms and Exclusions
ESD flooring warranties usually exclude moisture, slab movement, new cracking, mechanical damage and performance changes caused by improper cleaning or footwear. We review those exclusions with the facility before the job is sold so expectations are clear.
- 20+ Years of Floor Coating Work
- Moisture Testing in Every Scope
- Free Written Estimates